
CNC Turned Parts: What Tolerances and Surface Finishes Are Realistic?
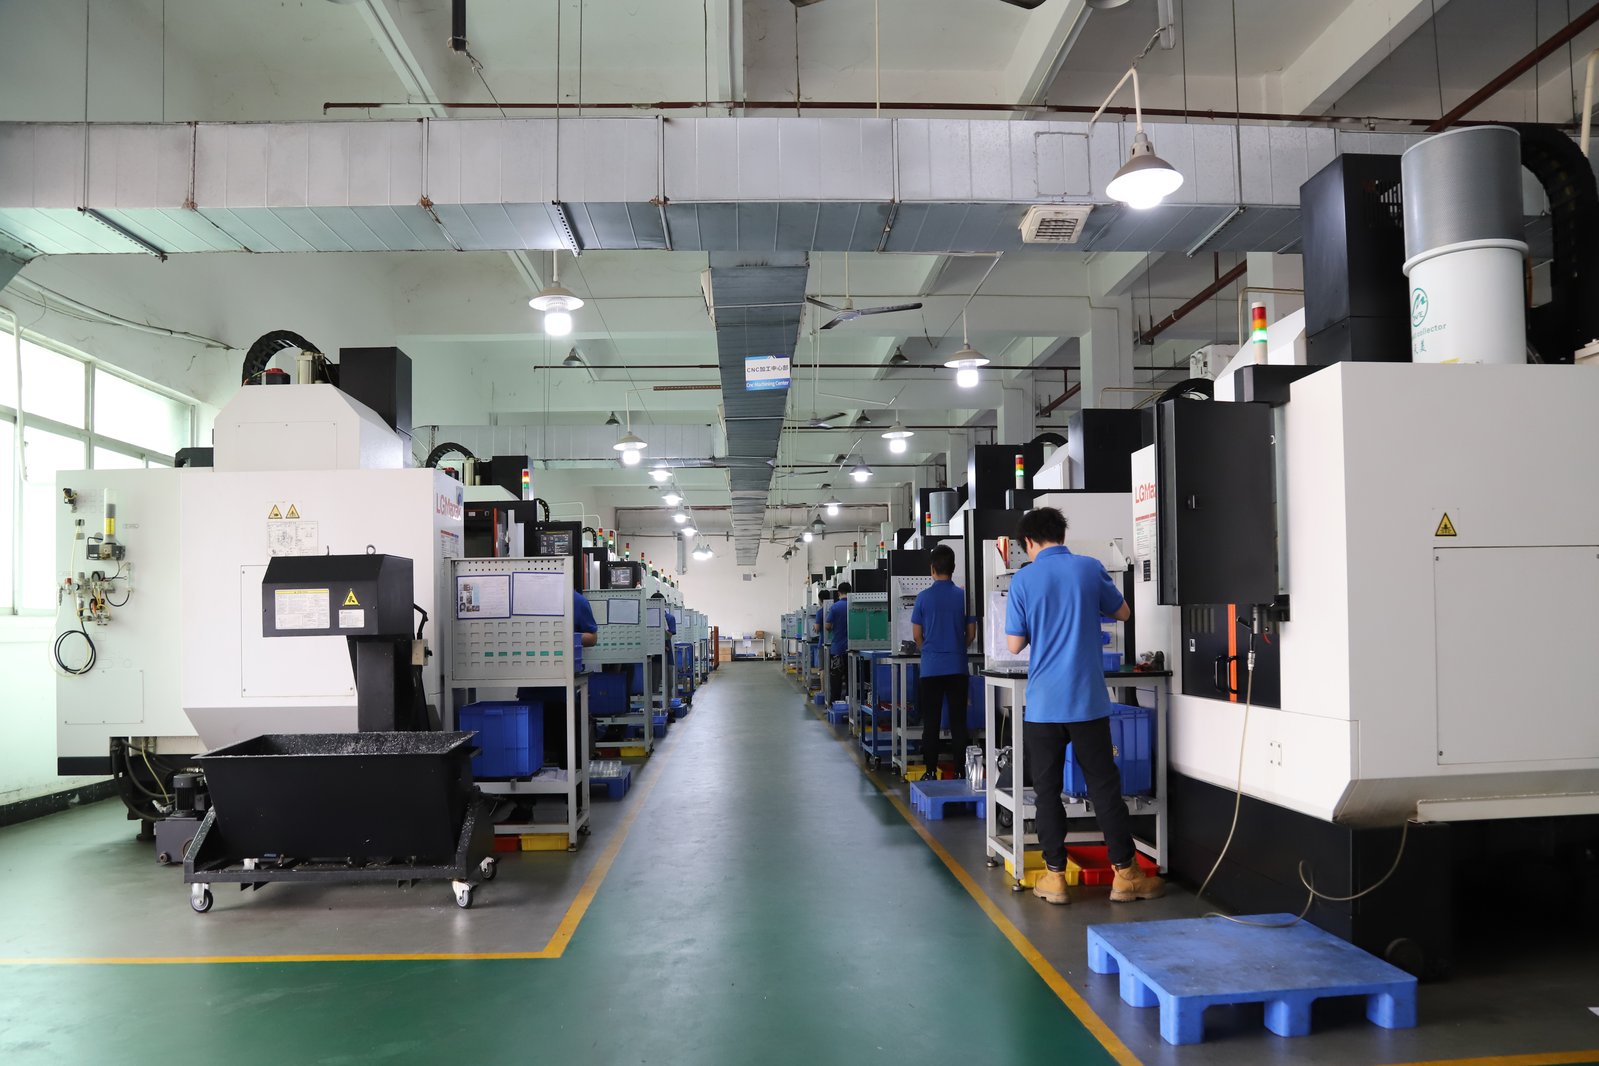
A tolerance is only realistic when a defined process can hold it across a run and a calibrated instrument can prove it on the parts you receive. Buyers usually ask it backwards — "what can you hold?" — before they have said what the feature must do. This guide gives the practical bands for CNC turned parts: what turning holds on a diameter, when a part stops being a turning job and becomes a grinding job, and which finish numbers belong on a turned surface. It closes with the records that make a tolerance claim worth the paper it is printed on.
Why is "what tolerance can you hold?" the wrong first question?
Every turned-part drawing carries two kinds of numbers: the ones that describe function and the ones that describe hopes. A shaft journal that carries a bearing, a bore that seals against an O-ring, a thread that takes a scheduled load — those earn a tight callout because the assembly fails without it. A cosmetic shoulder that nothing touches does not need one. The shops that quote honestly price the difference; the drawing that blurs the two pays for precision on surfaces that never use it.
So the realistic conversation starts with function, not with the smallest number a machine can hit. State what the feature does in the assembly — rotate against a seal, slide in a bore, carry a press fit — and the tolerance band follows from that, not from what impresses in a sales call. This is the same discipline behind the factory's verifiable capability claims: a number is worth quoting only when the process behind it is named and the inspection behind it is real.
What tolerance can CNC turning actually hold on a turned diameter?
CNC turning on a capable, thermally stable lathe holds a critical turned diameter to ±0.003 mm in production. That is not a laboratory figure on this floor: it is the stated working band for turning. It is kept honest by a process-capability target of Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window. — meaning the process spread sits inside the tolerance band with measurable margin for tool wear and temperature drift. Standard machining practice lines up with this: general CNC work is quoted near ±0.05 mm, precision features near ±0.02 mm, and high-precision seats, seal grooves, and bearing surfaces at ±0.003 mm.
Two limits keep that number honest. First, ±0.003 mm is a per-feature claim, not a whole-part claim. A lathe holds a short, rigid, single-setup diameter far better than it holds a length measured across two chuckings or a feature cut after the part was repositioned. Second, the band assumes the material behaves — a free-machining steel or 6061 aluminum turns to size predictably, while a gummy 304 stainless or a work-hardening titanium fights the tool and widens the real spread. When a shop quotes ±0.003 mm, the correct follow-up is not a discount; it is "which features, in which material, held how, measured with what?"
When does a turned part stop being a turning job and become a grinding job?
There is a clean dividing line on any turned component: features that need ±0.002 mm, or surface finishes that need to go below what a single-point tool leaves, move out of the lathe and into precision grinding. On this floor the turning band is ±0.003 mm and the grinding band is ±0.002 mm — the difference is not a smaller step of the same process but a different process family with its own machine, its own wheel dressing, and its own measurement step.
Grinding earns its place when the function demands it: a ground seat that seals a hydraulic piston, a journal that runs in a precision bearing with controlled roundness, a hardened part that turning cannot cut economically, or a finish below roughly Ra 0.4 µm that a tool-nose radius cannot generate consistently. When a drawing calls ±0.002 mm or a sub-0.4 µm finish on a functional surface, expect the quote to name grinding, and expect the shop that quotes it to hold a grinder on the same certified floor rather than silently subcontracting the step. The cost side of that crossing is laid out in the CNC turned parts cost model, where tolerance and finish are priced as process steps rather than wishes. The same logic runs the other way: a clearance diameter at ±0.05 mm with a general 1.6 µm finish should never pull a grinding operation into the route, because that is money spent on a process the function does not need.
What surface finish is realistic for CNC turned parts?
Surface finish on a turned part is written as Ra — the arithmetic average of the profile height in micrometers — and it is produced by the cutting geometry, not by polish. The feed rate and the tool nose radius set the height of the helical tool marks a turning pass leaves behind. That is why finish is a process decision: to move a turned surface from Ra 1.6 µm toward Ra 0.8 µm, the programmer drops the feed or swaps in a larger-nose-radius insert, and the cycle time rises with it.
| Ra callout | What it means on a turned part | Process that realistically delivers it |
|---|---|---|
| Ra 3.2 µm | Lightly machined or non-critical surfaces; visible tool marks acceptable | Rough-to-finish turning pass, no extra operations |
| Ra 1.6 µm | General machined surface for most functional and visible faces | Standard finishing turning pass |
| Ra 0.8 µm | Fine finish for sealing faces, bearing seats, and wear surfaces | Controlled finishing pass at reduced feed, or grinding where size is tight too |
| Ra 0.4 µm and below | Smooth enough for sliding seals and precision fits | Grinding, honing, or a polishing step; rarely a single turning pass on production |
Turned parts are often slightly smoother than milled ones at the same effort because the workpiece rotates past a fixed point, which produces a consistent helical lay rather than a grid of interrupted cuts. On this floor, as-machined turned surfaces commonly land between Ra 0.8 and 1.6 µm depending on the operation, and grinding reaches the finer end of the chart. The practical rule for a buyer: put Ra 0.8 µm or tighter only on the faces where function needs it, and let the rest ride on a general 1.6 µm note — otherwise the quote carries a finishing pass on surfaces nothing will ever touch.
Why do roundness, cylindricity, and concentricity matter more than the size callout on turned parts?
A turned part is a body of rotation, so its useful geometry is not just the diameter — it is how round that diameter is, how cylindrical it stays along its length, and how true one diameter runs to another. Two parts can both measure on-size at every diameter and still fail in the machine because one is slightly oval, or tapered, or running off-center between its two ends. These form errors are measured as roundness, cylindricity, runout, and concentricity, and on rotating parts they are often the callouts that decide whether the assembly works.
Realism here follows one master rule: features machined in a single setup hold their relationships to one another; features that require a re-chuck depend on the accuracy of that second clamping. A shaft turned complete in one chucking keeps its diameters concentric within the machine's own repeatability. Split the same part across two operations and the concentricity claim now includes the chucking error of the second setup. That is why mill-turn machining matters on turned parts: complex features that would force a second operation are cut in one clamping, and the geometric relationships stay as good as the machine, not as good as the setup crew.
How do material and geometry change what a turned part can hold?
Material is the quiet half of any tolerance conversation, because it decides how the chip forms and how much the tool pressure disturbs the part. Free-cutting grades — 12L14 steel, 303 stainless, C360 brass — cut clean, break short chips, and hold a diameter and a finish with a comfortable process spread. Aluminum 6061 turns predictably and finishes well. On the demanding end, 304 and 316 stainless work-harden and tear, and titanium runs slow and springy; the same callout that a brass part holds all day becomes a fight in titanium, and the honest shop widens the band or quotes the extra pass that closes it.
Geometry sets the second limit: stiffness. A short, stocky bushing clamped near the cut holds a tight diameter without argument. A slender shaft whose length runs many times its diameter deflects under the tool and springs back — the shop supports it between centers or with a steady rest, and the process changes before the number can hold. A thin-walled tube distorts as the chuck jaws clamp it, and the part leaves the machine round only to relax out of round when it is unclamped. When a drawing puts a tight callout on a long, thin, or thin-walled turned feature, the realistic response is not a smaller number but a conversation about support, stock, and clamping — the mechanics of holding the feature while it is cut.
Which surface finish and tolerance should you actually put on the drawing?
The drawings that quote cleanly and arrive on spec share one habit: they call out tight numbers only on features that carry function, and they let a general note cover everything else. Put the tolerance on the journal that fits the bearing, the bore that seals, the thread that takes the load, and leave the cosmetic shoulders and clearance diameters on a sensible general band. Put the Ra value on the sealing face and the sliding surface, and let the rest default to general machining finish.
There is a second discipline that keeps the quote realistic: state the measurement expectation with the callout. A tight diameter without a stated inspection method invites the cheapest measurement; a diameter called at ±0.003 mm with a CMM report or a calibrated micrometer reading named in the RFQ tells the shop exactly what proof ships with the parts. When tolerance and finish are both critical on the same feature, say so in one place — the shop can then plan the sequence that holds size and finish in the same pass, instead of discovering the conflict after the first article. For threads, keyways, and grooves, name the standard you expect — a thread class, a keyway width, a groove depth — because those features carry their own tolerance systems that no general band covers.
What records should arrive with the parts to prove the tolerance and finish?
A tolerance claim becomes a fact only when the record exists. The realistic package for a turned part order names the material, the process, and the measurement together. Material is confirmed by a mill certificate checked against the incoming lot — the floor behind this site XRF-verifies every lot against its certificate before the bar reaches a lathe. Size is confirmed by the inspection report — CMM results on the features you called tight, tied to the lot number on the packing slip. Finish is confirmed by a profilometer trace if you called an Ra value, because roughness is a measured profile, not a look. Process stability is confirmed by the SPC record — the Ppk ≥ 1.67 initial figure on key characteristics means the capability is demonstrated from a running process, not claimed from a brochure. The quality system behind these records is registered and auditable: ISO 9001:2015 (certificate 116024/A/0001/UK/En), IATF 16949:2016 (product design excluded) (131941/A/0001/SM/En), and ISO 14001:2015 (116024/B/0001/UK/En), held by the legal entity Dongguan Zhuohang Ltd (registration 91441900MA4UWT6X39). The quality page describes how a buyer audits that record set from a distance; the short version is that reports which ship with the batch, tied to the lot, are worth more than reports produced on request after delivery.
How do you turn a tolerance conversation into a first article that settles it?
The cheapest way to learn what a shop can actually hold is one part ordered on the real drawing. Because the floor here runs a MOQ of one piece, the first article compresses the whole question into a single shipment. One part carries the material certificate and XRF check, the machining route, the CMM report on the tight features, the roughness reading on the finish callouts, and the lot linkage that ties the paperwork to the part. Order the prototype at the same tolerances as production, inspect it against the drawing with the same instruments you will use for the release lot, and the tolerance conversation stops being a negotiation and becomes a measurement.
What the first article cannot tell you is process stability, that is what the run tells you, through the SPC chart and the Cpk value. A first article proves one part can be made; a capability record proves a process can make the thousandth one the same way. Read them together: the first article against the drawing, the SPC record against the tolerance band, and you have moved from "what is realistic?" to "what has been demonstrated?", which is the only version of the question that protects a production order.
Frequently Asked Questions
What is the standard tolerance for CNC turned parts?
General CNC machining is commonly quoted near ±0.05 mm, with precision features near ±0.02 mm. On critical turned diameters that carry function — bearing seats, seal grooves, locating surfaces — a capable turning floor holds ±0.003 mm in production, and precision grinding extends the band to ±0.002 mm where the function truly needs it.
What is a realistic surface finish for turned parts?
As-machined turned surfaces commonly land between Ra 0.8 and 1.6 µm depending on the operation, which suits most functional faces. Ra 0.8 µm is a fine finish for sealing and bearing faces; Ra 0.4 µm and below moves the part toward grinding, honing, or polishing and should be reserved for surfaces that genuinely need it.
Can CNC turning hold ±0.003 mm on every feature?
No. ±0.003 mm is a per-feature claim for short, rigid, single-setup diameters on material that cuts predictably. Long slender sections, thin walls, re-chucked features, and difficult alloys widen the real spread, and an honest shop widens the band or changes the process rather than quoting hope.
Does a tighter tolerance always cost more?
Only when it changes the process or the inspection. A clearance diameter moved from ±0.1 mm to ±0.05 mm may cost nothing if the same pass holds it anyway. Moving a feature from turning at ±0.003 mm to grinding at ±0.002 mm changes the process family, adds an operation, and legitimately moves the price. Spend the tight numbers on function, not on the whole drawing.
When should I specify grinding instead of turning?
Specify grinding when the function needs ±0.002 mm, a finish below roughly Ra 0.4 µm, a controlled roundness on a running surface, or a hardened part that turning cannot cut economically. If none of those apply, a finishing turning pass is the realistic route and the cheaper one.
What is the difference between Ra and Rz on a turned part?
Ra is the average roughness across the measured profile; Rz is the average height of the highest peaks and deepest valleys. Ra is the common callout for machined surfaces. Rz earns a place when peak behavior matters — a sealing face where a single tall peak can leak even when the average looks fine.
Why does the same tolerance cost different amounts at different shops?
Because the tolerance is not the product — the process that holds it is. One shop holds ±0.003 mm on a capable lathe with SPC evidence; another shop quotes the same number on worn equipment and sorts the results at inspection. Sorting is not capability, and the difference shows up in the rejection rate of your production order, not in the first quote.
What should I send with an RFQ for a tight-tolerance turned part?
Send the drawing with the functional callouts marked, the material grade named, the measurement expectation stated — CMM report, micrometer reading, or profilometer trace — and the general tolerance and finish notes explicit. A defined request is how you get a defined quote, a defined first article, and a tolerance you can verify on arrival rather than argue about after the fact.
What tolerances and finishes does your turned part actually need?
Send the drawing to [email protected] or call +86 13126536955 — the review comes back with the realistic process route, the tolerance band per feature, and the inspection record that will prove it.